
Views: 0 Author: Site Editor Publish Time: 2026-10-29 Origin: Site
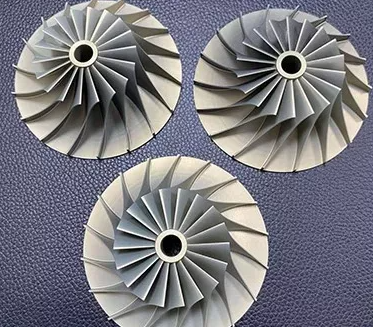
The five most common precision CNC machining processes are CNC milling, CNC turning, CNC drilling, CNC grinding, and CNC EDM. Precision CNC machining uses computer-controlled tools to cut or shape material and keep exact measurements each time. In 2021, the global market for this work reached USD 90.4 billion. Experts project it will grow at 8.4% per year through 2033. Each part below explains how a process works, its usual tolerances, materials, uses, and trade-offs. For projects needing one-stop support, Best Prototypes provides CNC machining, 3D printing, sheet metal, vacuum casting, injection molding, die casting, and post-processing finishes.
CNC milling is a way to cut flat and curved surfaces very accurately using a spinning tool.
CNC turning spins the workpiece to make cylinder-shaped parts like shafts and pins.
CNC drilling makes exact holes fast for screws and fluid paths.
CNC grinding and EDM give the tightest tolerances and the smoothest finishes for hard materials.
Pick a machining process based on the part's shape, material, tolerance, and how many you need to make.
CNC milling is a subtractive machining process. A spinning multi-point cutter takes material away from a workpiece that moves against it. Each tooth on the cutter goes into the material, cuts a chip, comes out into air to cool, and then goes back in. This stop-and-go cutting is what makes milling different from turning, where the workpiece spins instead of the tool.
The tool spins while the workpiece moves in X, Y, and Z. This motion lets the cutter make flat, angled, and curved surfaces. Face milling creates wide flat surfaces like mounting and sealing faces. Peripheral milling cuts side surfaces, steps, and shoulders. Angle milling forms chamfers and dovetails. Form milling makes concave or convex shapes. Contour milling follows programmed toolpaths to cut complex 3D profiles like housings and molds.
CNC milling works with aluminum, stainless steel, titanium, specialty alloys, and plastics. Both 3-axis and 5-axis milling hold tolerances near ±0.005 in. (0.13 mm), with a standard surface finish of 125 Ra. Thermal expansion and brittleness can change the tolerances you can reach, and tighter limits raise cost and inspection effort.
Aerospace work includes turbine blades, brackets, and structural fittings. Automotive production covers engine parts, transmission housings, and suspension components. Medical manufacturing mills surgical instruments, orthopedic implants, and dental prosthetics, often from biocompatible titanium.
The process offers versatility and tight tolerances, but setup cost and tool wear limit small batches. Entry-level CNC machines cost $60,000–$80,000, and 5-axis centers often exceed $200,000. Five-axis machining carries hourly rates of $150 to $325, roughly double or triple the $75 to $125 rate of standard 3-axis machines. For complex parts, fewer setups often offset that premium through less scrap and rework.
CNC turning is the opposite of milling. The workpiece spins while a still cutting tool shapes it. A chuck or collet holds the stock, and the spindle turns it at a set speed. The tool moves along the X-axis to set diameters and the Z-axis to set lengths and axial features.
Turning takes material off the outer area of the workpiece. The cutting tool moves in and out of the workpiece, changing depth to make contours or steps. Turning is done parallel to the workpiece's rotational axis (straight turning) to make straight cylindrical features or at an angle to the surface (tapered turning), creating tapered conical features.
Threading cuts spiral grooves around the circumference. The tool starts at the thread's beginning and moves sideways as the part spins. The CNC program controls speed and movement to hit accurate thread depth and pitch. A CNC lathe can cut both internal and external threads. Mill-turn machines with live tooling add milling features without a second setup.
CNC turning works with aluminum 6061 and 7075, stainless steel 303 and 316, brass C36000, titanium Grade 5, and engineering plastics like PEEK, Delrin, and PTFE. Standard tolerances sit near ±0.13 mm. General industrial work holds ±0.025 mm to ±0.05 mm, and precision work reaches ±0.005 mm to ±0.01 mm.
Category | Details |
|---|---|
Common materials | Aluminum, stainless steel, brass, titanium, engineering plastics |
Typical tolerances | Standard ±0.13 mm; general industrial ±0.025–0.05 mm; precision ±0.005–0.01 mm |
Applications | Shafts, pins, spacers, bushings, hydraulic fittings, valve stems, threaded inserts, motor shafts |
Turning works best for parts with rotational symmetry. Shafts, pins, bushings, spacers, and threaded components are common. High-volume work covers oil and gas components, threaded fasteners, and hydraulic cylinder parts. Swiss-type machines handle small-diameter aerospace fasteners and hydraulic fittings.
The process gives high repeatability. The computer controls every curve and contour, so each part matches the last. Features cut in one setup keep excellent concentricity. Non-cylindrical shapes and prismatic features need milling instead. Tool access near chuck jaws is limited, and thin-walled parts can deform under clamping force.
CNC drilling uses spinning drill bits to make holes with exact depth and position. The spindle turns the bit, and the machine moves it down the Z-axis. This process is used for fasteners and fluid passages.
Spindle speed and feed rate control hole quality. Bad settings cause heat, vibration, and stress that break the bit. Good settings reduce burrs, smooth the entry and exit, and make tools last longer. A spotting drill stops the bit from wandering on curved surfaces. Short overhang and slow entry feed help the point center itself. The CNC program controls movement for repeatable results.
Cycle choice matters for deep holes. Shallow holes up to 3xD run without pecking. Soft metals with long chips need chip break cycles. Deep or blind holes need full peck cycles to clear chips. The process makes through-holes, blind holes, and tapped holes. Tapped holes need a tap-size hole first; a tap or thread mill cuts the thread.
The process works on metals and plastics, from aluminum to titanium and composites. Hard metals make tools wear faster; soft plastics may bend. Coated carbide bits and through-tool coolant help with tough alloys.
Hole type | Typical tolerance/control |
|---|---|
Through hole | ±0.003–0.005 in. when drilled; reaming or boring makes it tighter |
Blind hole | Similar diameter tolerance; depth control is measured separately |
Tapped hole | Controlled by thread class, not the drilled-hole diameter |
Positional accuracy usually reaches ±0.01–0.05 mm. Modern CNC machines hold repeatability down to ±0.001–0.005 mm. Today's CNC equipment keeps these limits in production.
CNC machining makes precise hole patterns for enclosures, engine parts, and tooling. Starter holes line up bolts in enclosure panels. Horizontal machines reduce handling and keep mounting holes consistent in engine blocks. Fixtures lock parts so the machine controls accuracy. This precision CNC machining method works well for high-volume production.
Among machining processes, drilling stands out for speed and repeatability. Tighter tolerances add machining and inspection time; engineers save tight limits for critical fits. Designers compare machining processes by shape, material, and cost. A CNC machining center can add milling or tapping in one cycle.

CNC grinding uses a spinning abrasive wheel to remove very small amounts of material. The abrasive grains on the wheel work like tiny cutting tools. They cut off chips much smaller than a milling cutter can make. This is real cutting, not just rubbing. Each pass takes off less than 0.005 mm, so the wheel smooths surface peaks instead of tearing them.
The shallow cut depth is the key to the results. A finishing pass often runs 0.0001–0.0005 in. deep. After the wheel reaches the target size, the operator adds sparkout passes at zero infeed. Elastic deflection in the machine and workpiece recovers during these passes, so the remaining material grinds away without extra programmed feed. This step improves roundness and size consistency. Superfinishing goes one step further. An oscillating abrasive stone with very light pressure removes the disturbed surface layer and leaves a plateau finish with an excellent bearing ratio.
Grinding works well for hardened steels, carbide, ceramics, superalloys, and other hard alloys that standard cutting tools struggle to machine. It holds dimensional tolerances up to ±0.001 mm (IT5 grade) and surface finishes as low as Ra 0.05 μm. The table below shows how it compares with milling on the same part features.
Parameter | CNC Grinding | CNC Milling (Finishing) |
|---|---|---|
Typical Ra Range | 0.2 - 1.6 µm | 1.6 - 6.3 µm |
Flatness Control | High (0.005 - 0.01 mm) | Medium (0.02 - 0.1 mm) |
Dimensional Tolerance | ±0.01 mm standard; ±0.002–0.005 mm high-precision | Mid-tenth-millimeter class |
Bearing surfaces, shafts, plates, dies, and cutting tools such as end mills and drills all benefit from this process. One manufacturer of hardened D2 steel dies used CNC grinding to remove material cleanly, extend tool life, and meet specifications without constant tool changes or scrap losses.
The trade-off is speed. Hardened steels above 50 HRC need slower feed rates and more frequent dressing. Heat-retaining alloys like nickel and titanium require reduced infeed and heavier coolant management. Tighter tolerances and finer finishes each add passes and inspection time. Proper stock planning upstream keeps grinding time and cost stable.
CNC EDM removes metal using electrical sparks instead of a cutting tool. A pulsed DC supply sends voltage across a small spark gap. This gap sits between an electrode and a conductive workpiece. The parts stay submerged in dielectric fluid. When the voltage hits a critical level, the fluid ionizes and forms a plasma channel. That discharge heats local material to about 8,000–12,000 °C. It melts or vaporizes tiny amounts. The plasma then collapses, and the dielectric washes away eroded debris. A servo system keeps the spark gap steady.
This thermal action sets EDM apart from every other CNC machining method. No cutter touches the part, so hardness and cutter entry angle no longer limit the cut. The process erodes conductive material without cutting force. This suits hard metals, intricate cavities, and fine internal corners. Wire EDM uses a thin wire as the electrode. Sinker EDM burns a shaped electrode into the workpiece. Both approaches run on CNC machines that control the spark gap, pulse timing, and electrode path.
EDM handles any electrically conductive material. Common choices include tool steels such as D2 and H13, stainless steels, titanium, tungsten carbide, copper alloys, and superalloys like Inconel, Hastelloy, and Monel. Wire EDM holds tolerances as tight as +/-0.0001 inches on parts up to 12 inches long, 10 inches wide, and 8 inches high. Qualified features often reach +/-0.0001 inches, and some work hits +/-0.0002 inches or tighter. Actual capability depends on geometry, material behavior, thickness, and inspection requirements.
Part Size Category | Maximum Length (mm) | Maximum Width (mm) | Maximum Height (mm) | Minimum Thickness (mm) | Tolerance |
|---|---|---|---|---|---|
Small Parts | 50 | 30 | 10 | 0.5 | +/-0.005 mm |
Medium Parts | 100 | 70 | 40 | 1.0 | +/-0.01 mm |
Large Parts | 500 | 300 | 150 | 5.0 | +/-0.03 mm |
Tool and die shops depend on this precision machining method for injection molds, stamping dies, and punches. Aerospace and automotive teams cut mission-critical components with ultra-tight tolerances. Medical manufacturers machine surgical tools and implants. The limits are real, though. Standard EDM needs a conductive workpiece, so ceramics and plastics such as ABS, PE, PP, and PLA will not work. Material removal runs slower than milling or turning. The rate drops even more when finer surface finishes are required. Electrode costs, wire consumption, and dielectric maintenance add ongoing expense.
Tolerance capability is the biggest thing that sets these processes apart. Standard CNC machining holds ±0.005 in. (0.13 mm), but precision CNC machining gets to ±0.002 in. (0.051 mm). Reamed holes go even tighter, to ±0.0005 in. (0.0127 mm). The table below shows what each process can achieve.
Process | Achievable Precision Tolerance |
|---|---|
CNC milling | ±0.0002 in. (±0.005 mm) |
CNC turning | ±0.0002 in. (±0.005 mm) |
Precision grinding | ±0.0001 in. (±0.0025 mm) |
Wire EDM | ±0.0001 in. (±0.0025 mm) |
How hard the material is changes what a shop can hold. Aluminum 6061-T6 machines at 90% machinability and stays stable in size. Stainless steel 304 drops to 45% and gets harder as it is cut. Inconel 718 falls to 12% and needs stiff setups with strong spindle power. Because of these differences, the same tolerance costs more in hard alloys than in soft ones.
Part geometry drives the first choice. Milling and turning remove material for most shapes. Drilling makes holes fast. Grinding gives fine finishes on hardened steel and carbide. EDM cuts hard, conductive parts with sharp inside corners that a milling machine cannot make.
Heat sensitivity matters too. Aluminum and Delrin expand a lot during cutting, so shops use flood coolant and stress relief to keep parts from shrinking out of tolerance. Titanium and stainless steel build up heat at the cutting zone, which makes tools wear faster.
Production volume shapes cost. Prototypes and low-volume runs favor milling and turning because programming investment pays back quickly. Medium-to-high volumes benefit from Swiss turning or turn-milling. Tight tolerances raise cost sharply: moving from ±0.1 mm to ±0.005 mm multiplies machining cost by ten or more.
Best Prototypes offers a range of CNC machining processes to match any project requirement. Their one-stop services cover prototyping through batch production.
Each process serves a distinct role. CNC milling uses rotating cutters for flat and curved surfaces. Turning rotates the workpiece for cylindrical parts. Drilling makes holes. CNC grinding uses an abrasive wheel for smooth finishes. EDM uses electric sparks to erode conductive material.
Choosing the best machining process depends on part shape, material hardness, needed tolerance, surface finish, heat sensitivity, production volume, and cost. These factors pick between general material removal and precision CNC machining.
Best Prototypes supports every step, from prototyping to batch production. Their one-stop services include 3D printing, sheet metal, vacuum casting, injection molding, die casting, and post-processing finishes. Contact them for project help.
CNC grinding and wire EDM reach the tightest limits. Grinding holds ±0.001 mm on hardened steel. Wire EDM cuts conductive parts to ±0.0001 in. For precision cnc machining, these two machining processes beat milling and turning on fine finishes.
Part shape comes first. Milling and turning remove most of the material. Drilling makes holes quickly. Grinding smooths hard steel. EDM cuts sharp inside corners. Each cnc machining process fits a different job. Engineers judge machining processes by shape, material, and volume.
No. Standard cnc machines have trouble with hardened steel above 50 HRC. Grinding and EDM work on those alloys instead. A shop picks the right cnc machining method for the material, since hard metals wear cutting tools down fast and raise machining cost.
Yes. Best Prototypes runs many types of cnc machines in one place. The team matches each cnc machining process to the part, then adds machining and finishing steps. This one-stop model covers prototyping through batch production for every cnc project.
Tighter limits raise cost quickly. Going from ±0.1 mm to ±0.005 mm can make machining cost ten times higher or more. Shops add inspection, slower feeds, and more passes. Engineers compare machining processes by tolerance, material, and volume. Simple cnc work stays cheap; tight-tolerance cnc work does not.


